In severe industrial pumping applications handling boiling sulfuric acid, thermal oils up to 400°C, or high-chloride seawater, casting integrity is the single point of failure. Porosity, uncontrolled ferrite-to-austenite ratios in Duplex steels, or improper trace element chemistry directly cause cracked volutes and catastrophic mechanical seal failures.
Established in 2018 to eliminate dependence on commercial casting jobbers, Flowline's captive steel foundry in Coimbatore guarantees 100% material traceability. Certified under ISO 9001:2015 and European Pressure Equipment Directive (PED 2014/68/EU Annex I, Sec. 4.3), every single heat undergoes optical spectroscopy and hydrostatic certification.
Direct foundry-to-plant manufacturing economics without trading intermediaries.
Heat-number stamped on every volute casing with EN 10204 3.1 Material Test Certificates.
Advanced equipment ensuring precision metallurgy for extreme temperature and aggressive chemical duties.
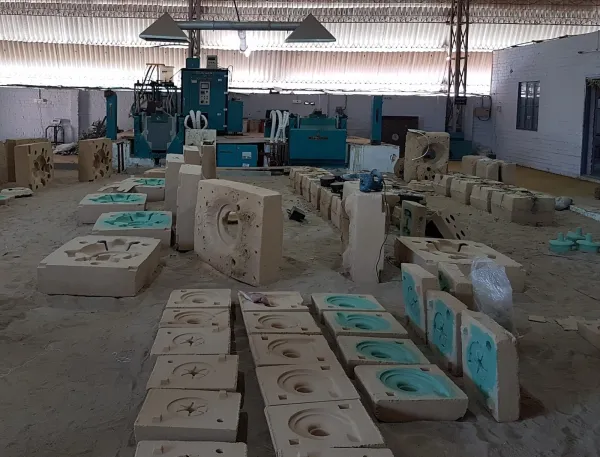
Medium-frequency dual crucibles capable of clean melting for CF8M, Duplex, and high-nickel alloys with resin sand moulds.
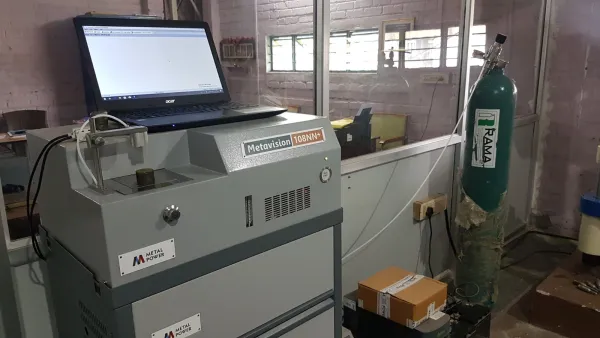
CCD-based optical emission spectrometry with real-time Nitrogen channel analysis to lock phase balance and PREN numbers in Duplex grades.
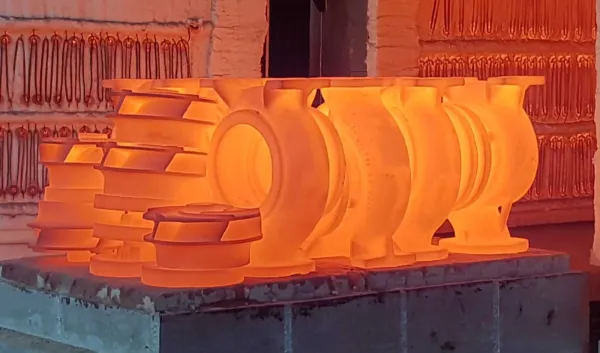
Water-quenching facility calibrated to API 6A Annex M, ASTM A991, and NORSOK M650 for solution annealing of stainless and Duplex steels.
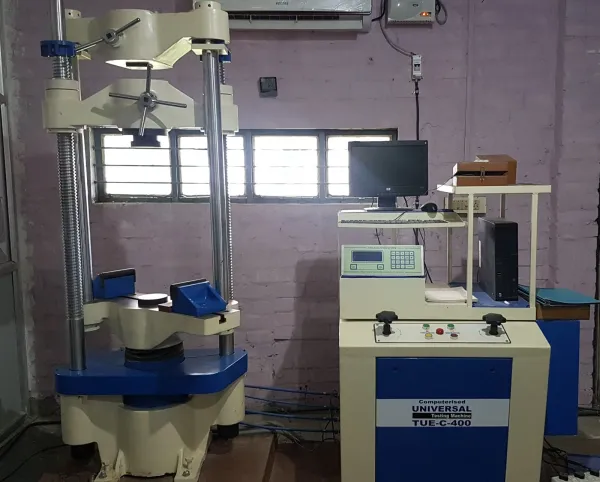
Tensile yield testing, elongation verification, and Brinell/Rockwell hardness testing on test bars poured alongside every production heat.
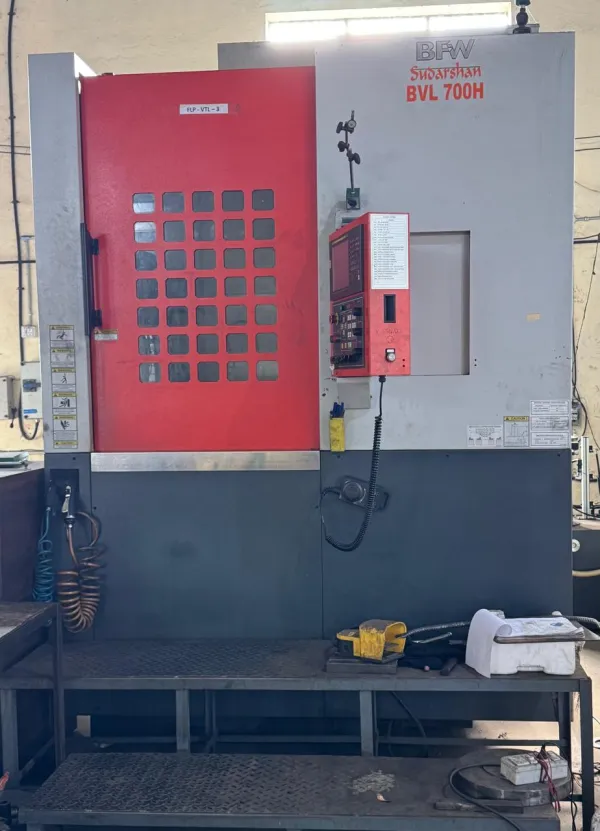
Rigid vertical lathe machining volute casing flange faces, stuffing boxes, and internal profiles with micron-level tolerances.
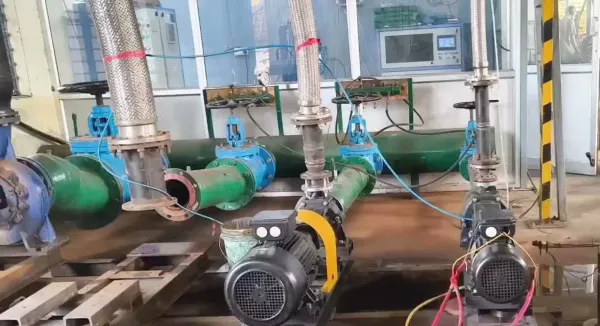
Every single volute casing, casing cover, and discharge head undergoes 1.5x design pressure hydrostatic testing prior to machine clearance.
From ductile iron for thermal oil duty to exotic high-nickel super alloys for severe corrosive service.
| Material Family | Standard ASTM / EN Specifications | Standard Testing Protocols |
|---|---|---|
| Ductile Iron / SG Iron | EN-GJS-400-15 (GGG-40.3), EN-GJS-500-7 | Microstructure nodularity check (>85%), Tensile, Hardness |
| Carbon Steel | ASTM A216 Gr. WCB, WCC | Spectro chemistry, Mechanical tensile, Radiography (RT) |
| Austenitic Stainless Steel | ASTM A743 / A351 Gr. CF8, CF8M, CF3, CF3M | Intergranular corrosion (ASTM A262 Practice E), Solution Annealing |
| Duplex & Super Duplex | ASTM A890 / A995 Gr. 1B (CD4MCuN), 4A (2205), 5A / 6A (2507) | Ferrite count (E562), Nitrogen analysis, Pitting resistance PREN > 42 |
| Super Austenitic / High Alloy | ASTM A743 Gr. CN7M (Alloy 20), SMO 254 (CK3MCuN) | Optical spectrometry, Critical pitting temperature (CPT) test |
| High Nickel Alloys | ASTM A494 CW12MW (Hastelloy C-276), CW6M, CZ-100 (Monel) | 100% Radiography, Positive Material Identification (PMI) |
Process plants frequently face 6-month lead times and exorbitant costs when sourcing replacement impellers, shafts, or casings for obsolete imported European or American pumps. Flowline’s Coimbatore facility specializes in rapid 3D optical laser scanning, CAD aerodynamic reconstruction, pattern making, and custom casting in elevated metallurgy.